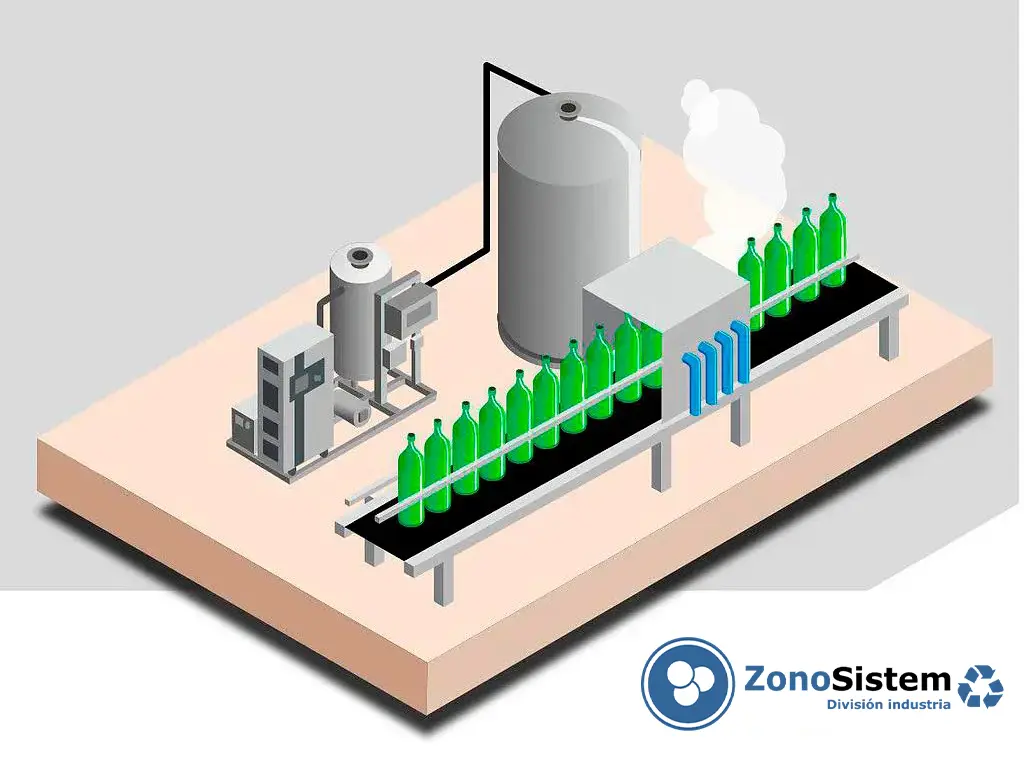
Use of ozone in a water bottling plant
An increasing number of companies are involved in the marketing of water-based soft drinks, that is, filtered and remineralised water that is bottled and sold. Ozonation technology is essential in this industry, as it enables the water to be disinfected without leaving any biocidal residues, without altering its composition or taste, and with a complete guarantee of hygiene.
As well as being an excellent biocide produced on site, it enables the removal of heavy metals and organic matter.
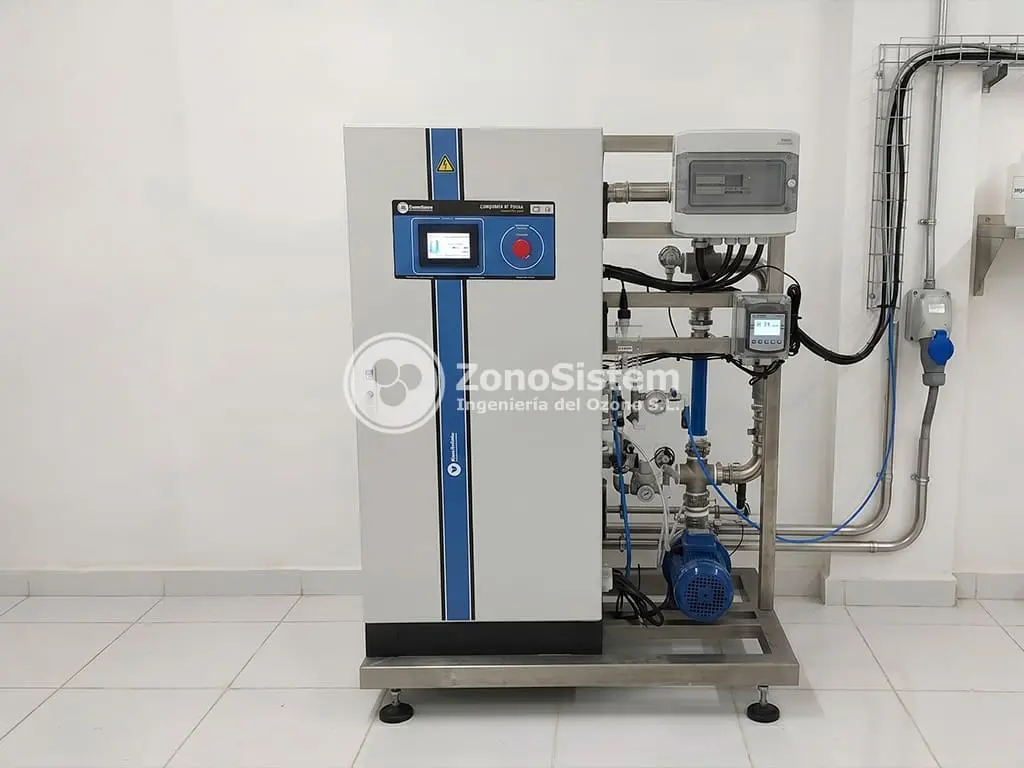
ZonoSistem manufactures compact ozonation systems designed for simple and efficient integration into this industry. These ozonation systems operate automatically, maintaining constant dosages and recording data.
Ozone generators for water bottling plants
Disinfects bottled water using residue-free technology
Ozone reduces the use of detergents, cold and hot water, and energy
Ozone is generated on-site; there is no need to store or transport chemicals
Ozone leaves no residue, does not alter the recipe and reduces waste
The system is automated; it does not require manual labour to operate
Why use ozone to disinfect bottled water?
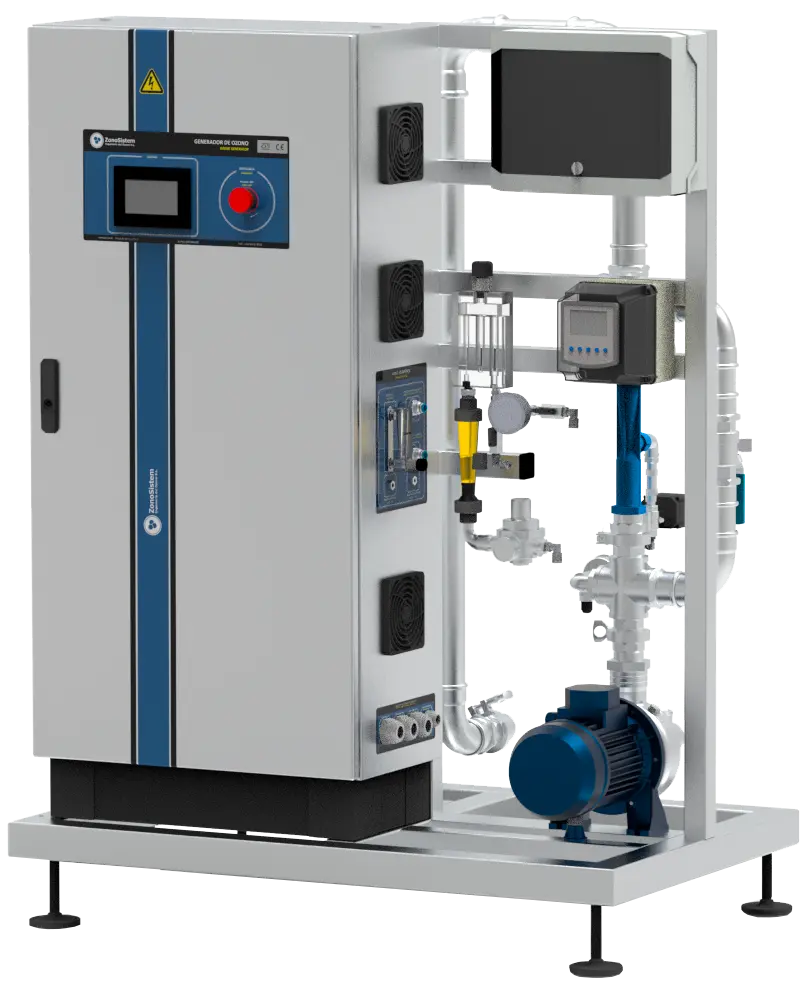
Optimise your production line with Zonosistem’s ozone technology, the advanced oxidation solution specifically designed to meet the demands of the drinks industry. As ozone is the most powerful natural disinfectant, this system eliminates the need for traditional chemicals and synthetic biocides, ensuring a stable biocidal process and full hygiene standards for bottle rinsing and CIP circuit disinfection.
Unlike chlorine or peracids, ozone rapidly breaks down into pure oxygen without leaving any chemical residues, which helps to prevent any alteration to the taste, odour or organoleptic properties of the final product. Its high oxidation potential acts selectively to break down the organic matter present in the process water and effectively precipitate heavy metals such as iron and manganese, ensuring water of the highest purity for bottling.
The deployment of this technology not only improves the technical quality of the product, but also helps to reduce its carbon footprint by minimising the transport of chemical packaging and eliminating the need for costly thermal rinsing. With the Zonosistem system, your bottling plant reaches a new level of sustainability and operational efficiency, transforming food safety into a profitable competitive advantage.
Optimise your production line with Zonosistem’s ozone technology, the advanced oxidation solution specifically designed to meet the demands of the drinks industry. As ozone is the most powerful natural disinfectant, this system eliminates the need for traditional chemicals and synthetic biocides, ensuring a stable biocidal process and full hygiene standards for bottle rinsing and CIP circuit disinfection.
Unlike chlorine or peracids, ozone rapidly breaks down into pure oxygen without leaving any chemical residues, which helps to prevent any alteration to the taste, odour or organoleptic properties of the final product. Its high oxidation potential acts selectively to break down the organic matter present in the process water and effectively precipitate heavy metals such as iron and manganese, ensuring water of the highest purity for bottling.
The deployment of this technology not only improves the technical quality of the product, but also helps to reduce its carbon footprint by minimising the transport of chemical packaging and eliminating the need for costly thermal rinsing. With the Zonosistem system, your bottling plant reaches a new level of sustainability and operational efficiency, transforming food safety into a profitable competitive advantage.
Why use ozone to disinfect bottled water?
Guaranteed water disinfection
Ozone is a powerful oxidising agent, and when dissolved in water it rapidly eliminates all types of pathogens, with a level of effectiveness far superior to that of conventional systems. It also keeps hydraulic surfaces disinfected, compared with UV.
Removal of heavy metals and organic matter
Ozone is effective at oxidising organic matter and heavy metals in water; it leaves no residue and ensures the highest water quality
No waste, no changes to your recipe
El ozono tiene un potencial de desinfección muy alto, pero tiene efecto residual bajo, es decir, no perdura en el tiempo. Se transforma en oxígeno pasado unos minutos y evita que tu receta pueda verse alterada.
More profitable and less risky
If you save on chemicals, water, time and energy every day, you’ll be reducing your operating costs and becoming more profitable. What’s more, if you reduce the risk of your products becoming contaminated by chemicals, your system will be more reliable and your customers will appreciate it.
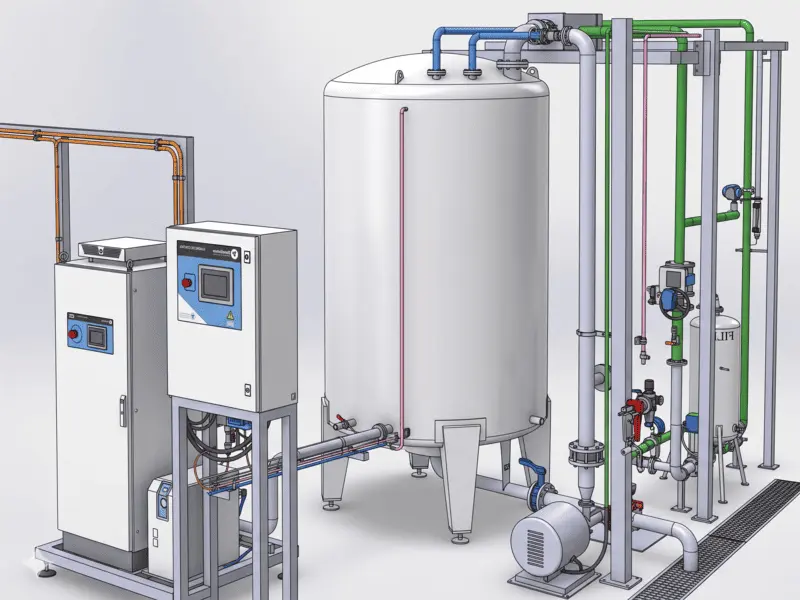
Ozone projects tailored to your needs
We design, manufacture, install and maintain comprehensive ozone systems for the disinfection of bottled water. Your project is in the best hands.
Contact us
Ozone projects tailored to your needs
We design, manufacture, install and maintain comprehensive ozone systems for the disinfection of bottled water. Your project is in the best hands.
Contact us
ZonoSistem case studies in the disinfection of bottled water
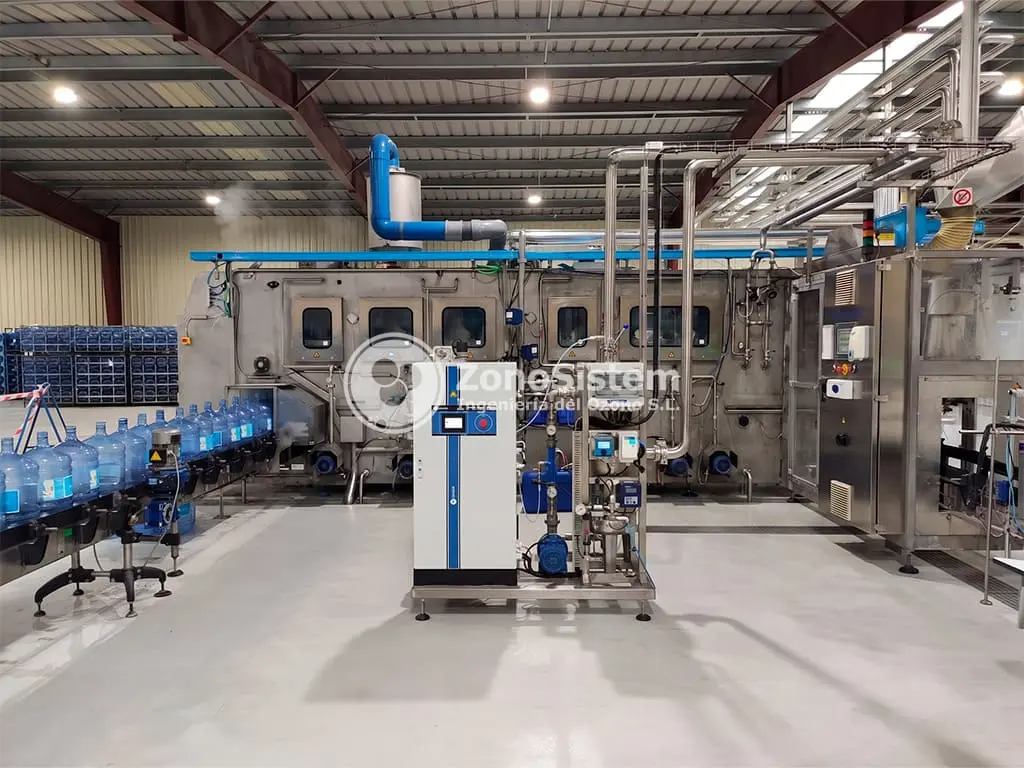
Ozone in a water bottling plant, Spain
The aim of the project is to disinfect the surface of reused water bottles without the need for a final rinse. To achieve this, highly concentrated ozonated water is applied, enabling disinfection on contact. The ozone system operates in a pressurised line using ZonoSistem’s HIDRO VT ozone systems, treating the rinse water as it passes through and transforming it into disinfectant water.
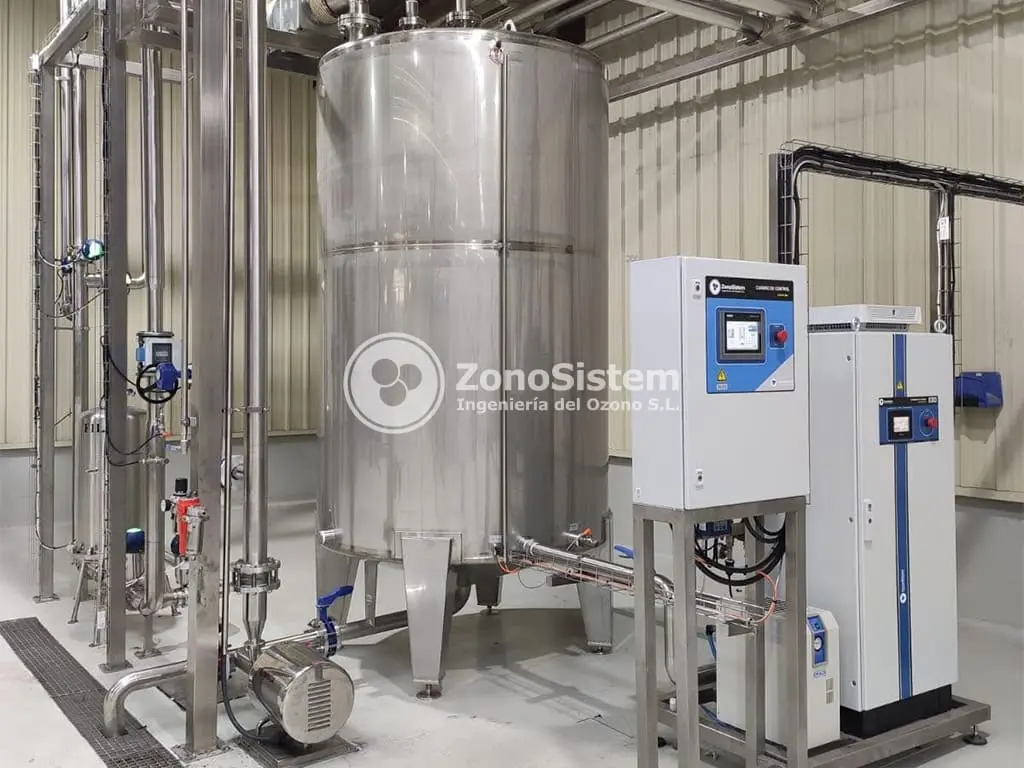
Ozone in a water bottling plant, Spain
The project includes a HIDRO V ozonation system from ZonoSistem, designed to disinfect the process water. To this end, an atmospheric tank is used through which 100 per cent of the bottling flow passes. The ozone maintains a constant dose and reliably disinfects the water. A control and monitoring system for dissolved ozone ensures the process runs smoothly, recording all data so that the quality system can certify the treatment. The project includes accessories that ensure process safety, such as residual ozone destroyers and degassing valves.
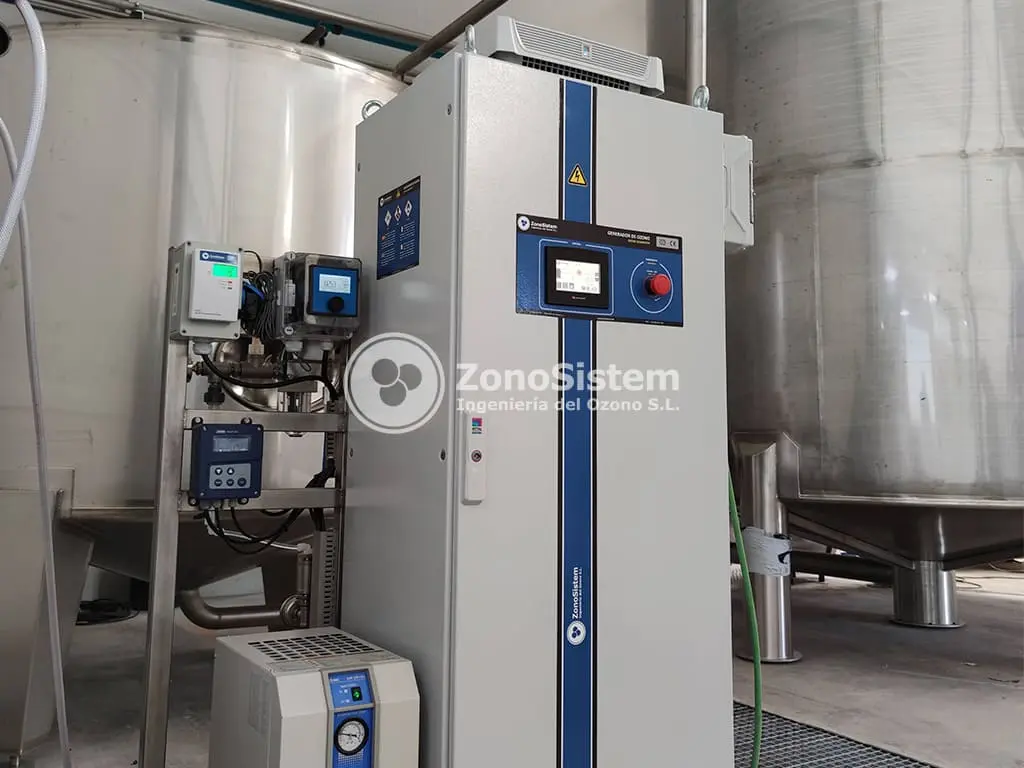
Ozone at a water bottling plant, Portugal
The project includes a HIDRO V ozonation system from ZonoSistem, which is designed to disinfect water for bottling. The soft drink (non-mineral) industry disinfects water with ozone after it has passed through the membrane filtration system and undergone mineralisation. Ozone is a key ally in ensuring safety and disinfection.
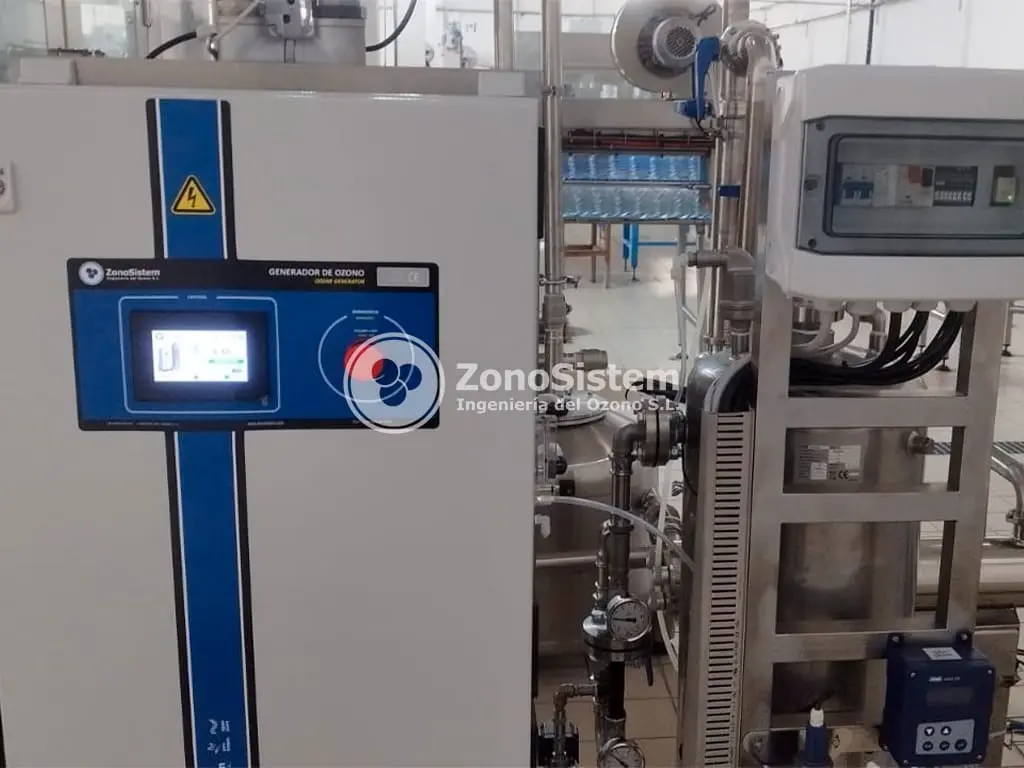
Ozone for water bottling, Senegal
The project involves disinfecting the water prior to bottling, with the aim of ensuring it is thoroughly disinfected. The water is natural mineral water sourced from a spring, but microbiological contamination in the tunnel makes it necessary to use ozone to disinfect the water without leaving any residues.
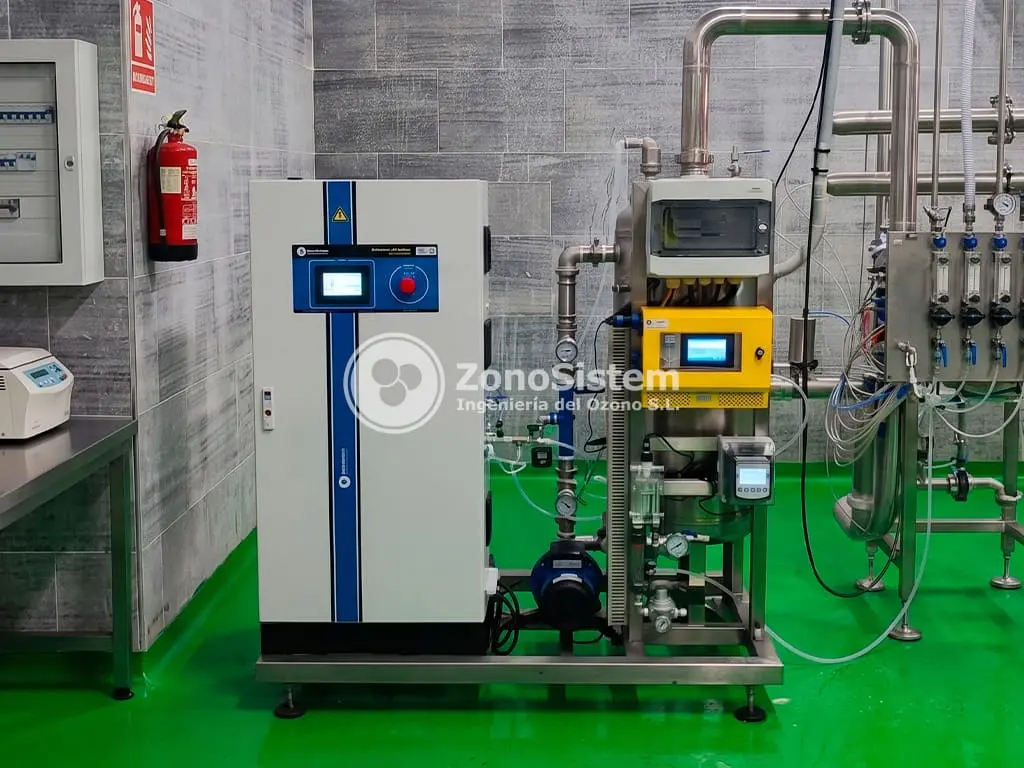
Ozone for a water bottling line, Cuba
HIDRO VT in-line water treatment system, pressurised for use in a bottling plant in Cuba. The ozone used in this project ensures that the water is disinfected without the need to treat storage tanks. An automated control system enables a constant dose to be maintained, even when water quality or flow rate vary.
Ozone in a water bottling plant, Spain
The aim of the project is to disinfect the surface of reused water bottles without the need for a final rinse. To achieve this, high-concentration ozonated water is applied, enabling disinfection on contact. The ozone system operates in a pressurised in-line configuration using ZonoSistem’s HIDRO VT ozone systems, treating the rinse water as it passes through and transforming it into disinfectant water.
Ozone in a water bottling plant, Spain
The project includes a HIDRO V ozonation system from ZonoSistem, designed to disinfect the process water. To this end, an atmospheric tank is provided through which 100 per cent of the bottling flow passes. The ozone maintains a constant dose and reliably disinfects the water. A control and monitoring system for dissolved ozone ensures the process runs smoothly, recording all data so that the quality system can certify the treatment. The project includes accessories that ensure process safety, such as residual ozone scavengers and degassing valves.
Ozone in a water bottling plant, Portugal
The project includes a HIDRO V ozonation system from ZonoSistem, which is designed to disinfect water for bottling. The soft drink (non-mineral) industry disinfects water with ozone after it has passed through the membrane filtration system and undergone mineralisation. Ozone is a key ally in ensuring safety and disinfection.
Ozone for water bottling, Senegal
The project involves disinfecting the water prior to bottling, with the aim of ensuring it is thoroughly disinfected. The water is natural mineral water sourced from a spring, but microbiological contamination in the tunnel makes it necessary to use ozone to disinfect the water without leaving any residues.
Ozone for a water bottling plant, Panama
Natural mineral water containing dissolved metals such as iron and manganese requires these to be oxidised using a technology that leaves no residue and is highly effective. The use of ozone enables the water to be disinfected and heavy metals to be removed prior to bottling, thereby ensuring water quality.
Ozone for a water bottling line, Cuba
HIDRO VT in-line water treatment system, pressurised for use in a bottling plant in Cuba. The ozone used in this project ensures that the water is disinfected without the need to treat storage tanks. An automated control system maintains a constant dose, even when water quality or flow rate vary.
Frequently asked questions about the use of ozone in the disinfection of bottled water
Ozone is used as a disinfectant to ensure the microbiological quality of the water throughout the bottling process. It eliminates bacteria, viruses and other microorganisms from the water, as well as from the production lines, tanks and containers, ensuring that the final product meets health standards without the need to add persistent chemical disinfectants.
No. When used correctly, ozone does not alter the organoleptic characteristics of the water. It breaks down rapidly into oxygen, so it leaves no residue and does not alter the taste, smell or composition of the final product, thereby maintaining the purity of the bottled water.
Ozone can be used at various stages of the process, such as disinfecting water prior to filling, sanitising bottles and caps, and cleaning lines and tanks (CIP). Its versatility means it can be easily integrated at various critical control points, thereby improving the plant’s overall microbiological safety.