Industrial Applications of Ozone
Ozone Treatment in Process Water
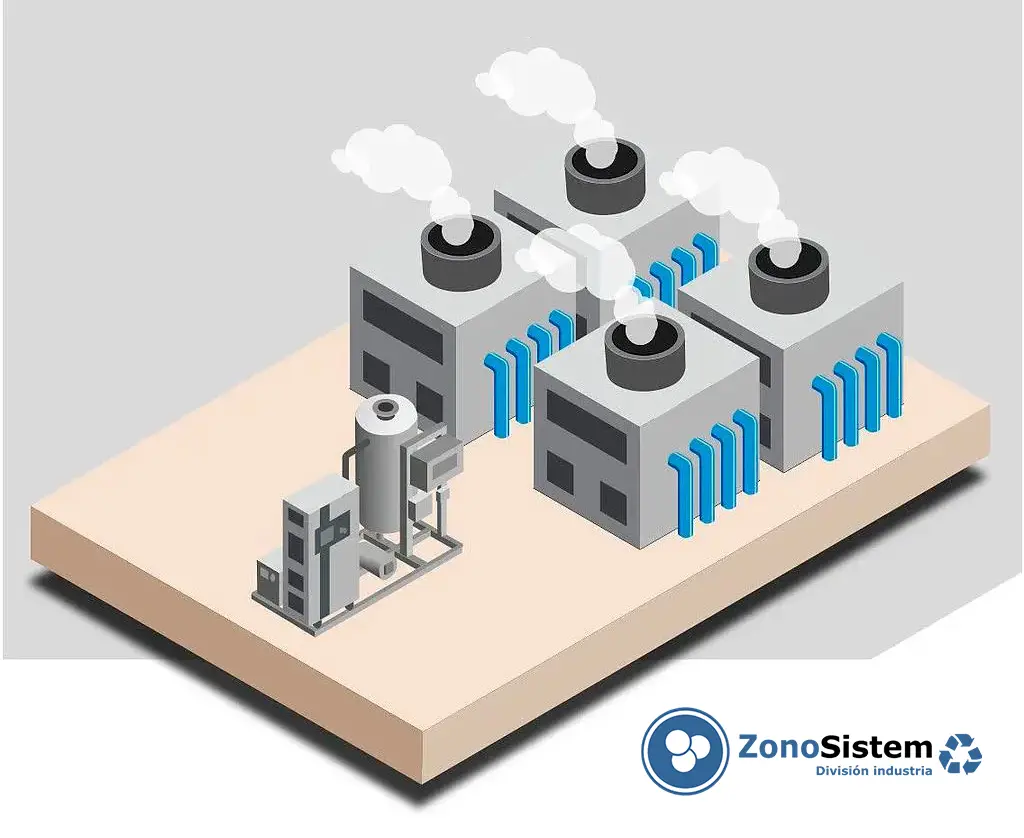
Ozone for cooling towers
Ozone has become a truly useful tool for disinfecting water in cooling towers, particularly in the fight against Legionella.
Ozone is neither stored nor transported. It is generated on site by the ozone generator and injected directly into the water in the cooling tower. As it passes through, the ozone rapidly and effectively eliminates all types of microorganisms, including Legionella.
The ozone generator operates automatically and requires no manual intervention; it simply draws in ambient air and electricity. It maintains hygiene in the water within the cooling tower, as well as in the ducts, pipes and basins. A disinfection technology that can be monitored in real time, with data logging, and also controlled remotely.
Ozone for CIP systems
Ozone has become a powerful tool for sanitising and optimising CIP (Clean-in-place) systems across all types of food and bottling industries. Ozone is a powerful disinfectant that eliminates all types of pathogens and biofilm from pipework. However, its real advantage lies in the savings it delivers: it reduces the consumption of chemicals and hot water, shortens processing times and reduces the number of rinses, whilst also lowering the volume and level of contamination in effluent.
Ele não deixa resíduos que possam afetar suas receitas ou produtos, o que proporciona aos clientes ainda mais tranquilidade. Além disso, o ozônio é gerado no local, portanto, não há necessidade de transportá-lo, armazená-lo ou manuseá-lo. O sistema opera de forma totalmente automática e não requer trabalho manual. Com o ozônio, você tem a garantia de desinfecção, com medições em tempo real, ao mesmo tempo em que desfruta de uma economia considerável em comparação com os sistemas tradicionais.
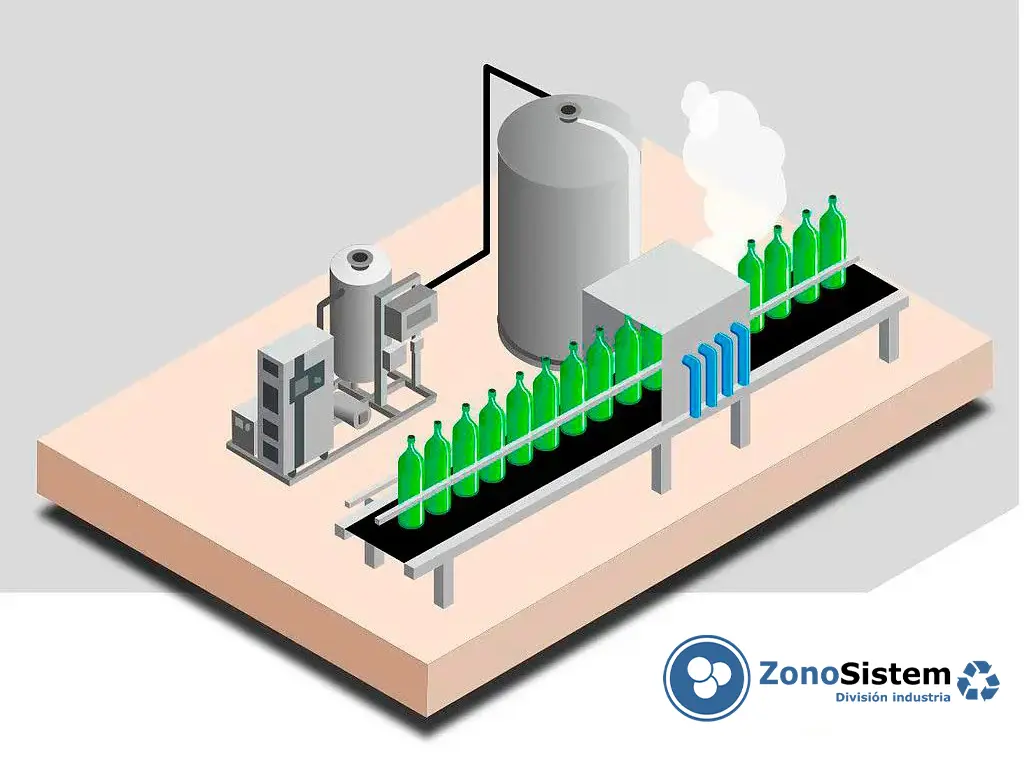
Ozone for bottled water
An increasing number of companies are involved in the marketing of water-based soft drinks, that is, filtered and remineralised water for bottling and sale. Ozonation technology is essential in this industry, as it enables the water to be disinfected without leaving any biocidal residues, without altering its composition or taste, and with a complete guarantee of hygiene.
As well as being an effective biocidal agent produced on site, it helps to remove heavy metals and organic matter.
ZonoSistem manufactures compact ozonation systems designed for simple and efficient integration into this industry. These ozonation systems operate automatically, maintaining constant dosages and recording data.
Ozone for osmosis-treated, ultrapure and distilled water
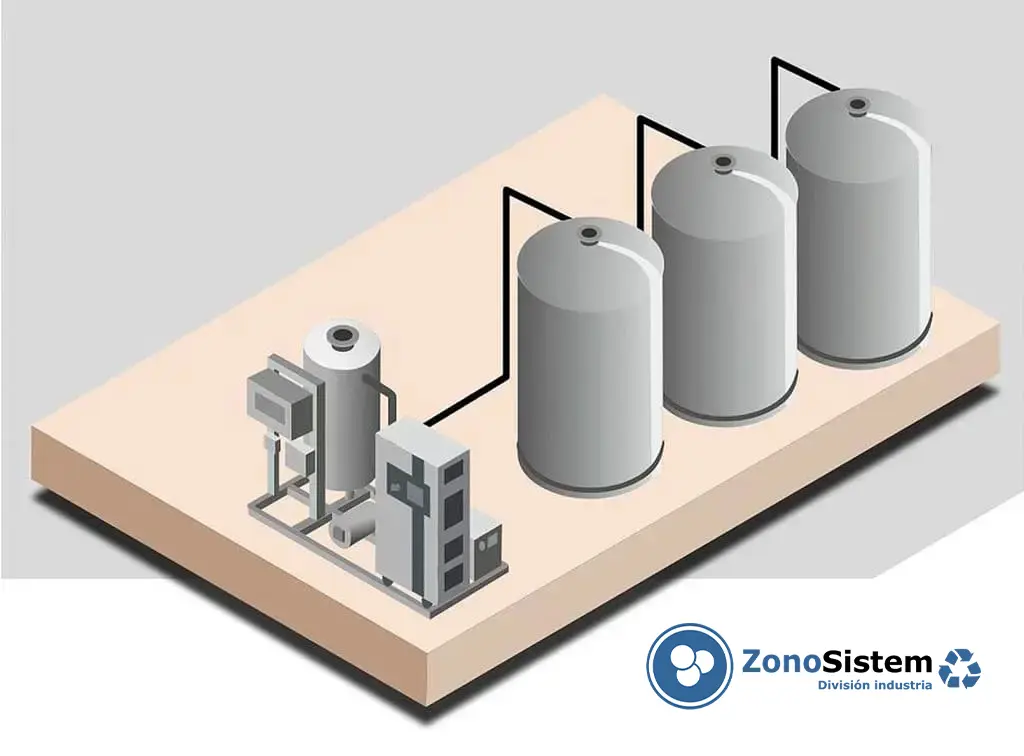
Osmotised, distilled and ultra-pure water is widely used in industry as a base for producing a wide range of formulations, in the manufacture of food, pharmaceutical, cosmetic, chemical and cleaning products, amongst others. If you store the water in a buffer tank, you will need a continuous disinfection system that ensures constant hygiene in the tank, the pipework and the water itself, whilst leaving no traces that could alter the taste, smell or composition of your product.
Ozone is a highly effective method for sanitising and disinfecting tanks, reservoirs, pipes and the water itself, without leaving any traces of chemicals that might alter its composition. Furthermore, as the ozone is generated on-site, there is no need to transport or store chemicals. The ozone generator extracts oxygen from the air, converts it into ozone using electrical discharges, and injects it into the water in the tank via its injection and contact system. The system only requires a power supply and to be connected to the tank you wish to treat. The system operates fully automatically, without the need for manual labour. It is also environmentally friendly.
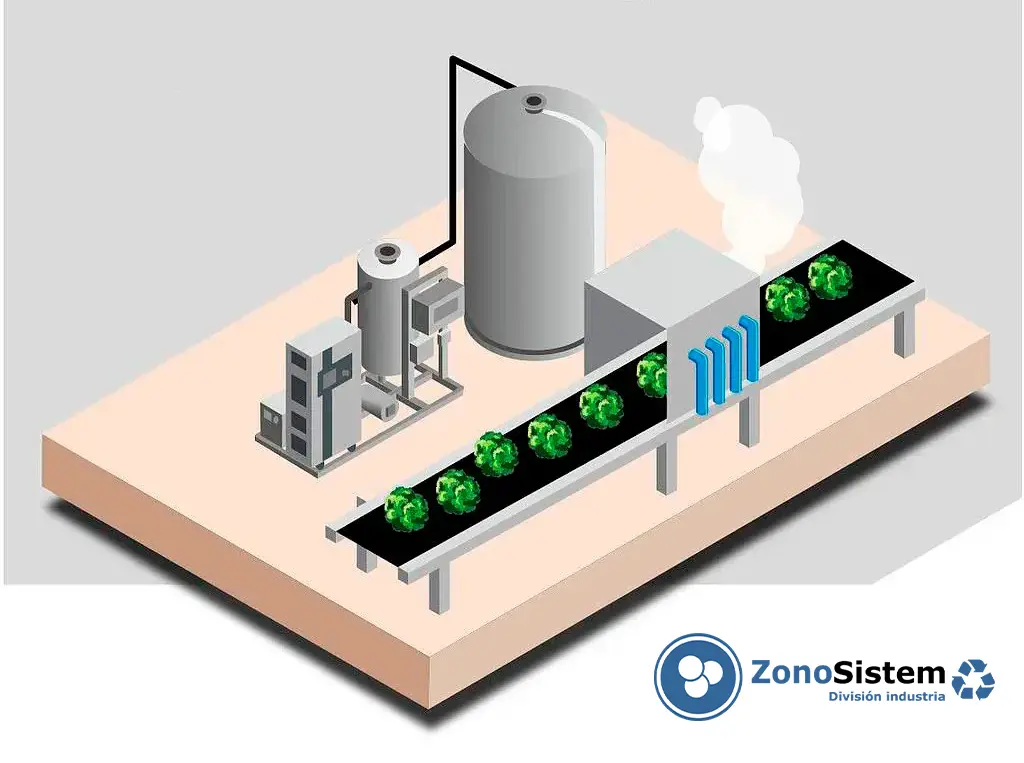
Ozone for fruit and vegetable washing facilities
Ozone is a powerful oxidising agent used to maintain hygiene and disinfect water in washing facilities for fruit and vegetables. The shelf life of vegetables depends largely on storage conditions and the microbiological load present on the surface of the produce.
During the washing process, the product may become contaminated with chlorites and chlorates, as stipulated by European regulations; this is why it is very important to maintain the hygiene and quality of the wash water. Ozone enables us to eliminate all types of microorganisms, with greater efficacy than traditional disinfectants. It also improves water quality, reducing COD, BOD, turbidity, organic load, odour, colour and taste, without leaving any residues that could alter the product’s organoleptic properties.
Ozone for industrial textile laundering
Ozone is a powerful oxidising agent which, when diluted in the wash water, delivers significant benefits for the business owner and the environment. Ozone enhances the action of detergents, thereby reducing detergent usage; furthermore, it shortens wash times and reduces the number of rinse cycles, thereby reducing water consumption and the volume of wastewater per kilogramme of laundry. In many cases, it also makes it possible to eliminate the need for hot water entirely, thereby considerably reducing energy consumption. All these advantages ultimately enable the business owner to save money per kilogramme of laundry, wash more kilograms per day, reduce the volume of effluent and lower the pollution level of the effluent per kilogramme of laundry washed, thereby optimising the process and making their laundry business more profitable and sustainable.
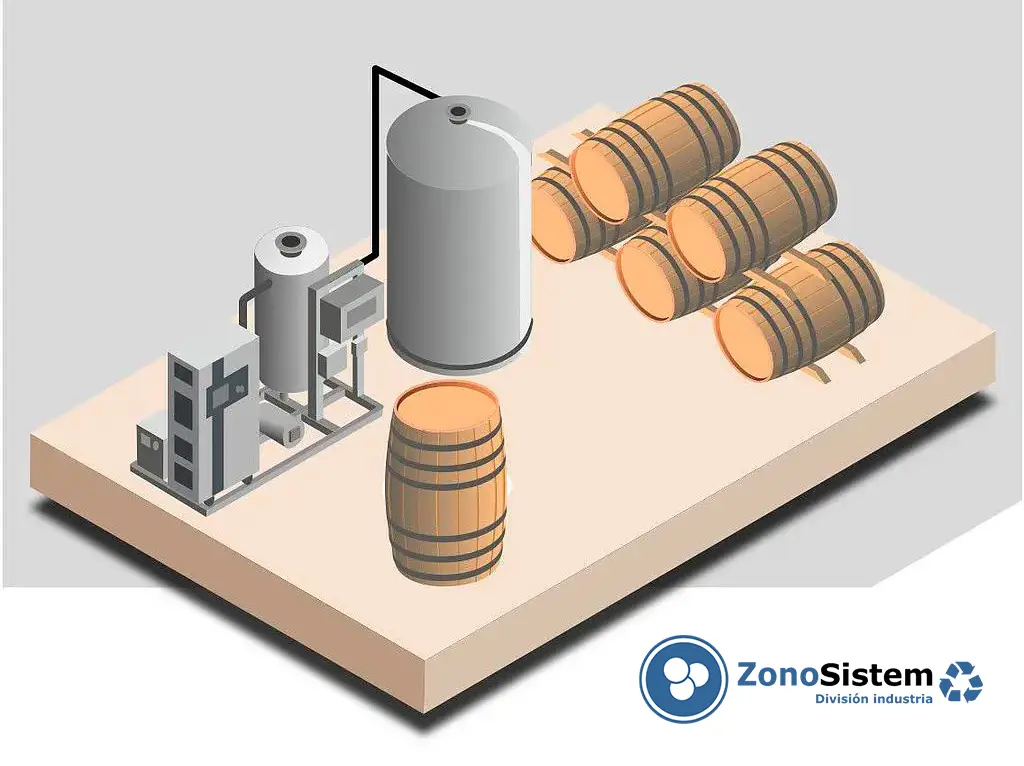
Ozone for wine barrels
Ozone, due to its powerful disinfecting properties, is used internationally in many wineries that favour rapid and efficient treatments without the use of chemicals. Ozone dissolved in the water used to wash the barrels, at the correct concentration and for the appropriate contact time, ensures the complete disinfection of the wood. Ozone is effective against viruses, bacteria, fungi, moulds and yeasts. It is also effective against resistant spores and does not need to be rinsed off once the process is complete. Ozone breaks down into oxygen once the process is complete and does not affect the quality of the wine to be stored in the barrel.
Fast, secure and efficient technology.
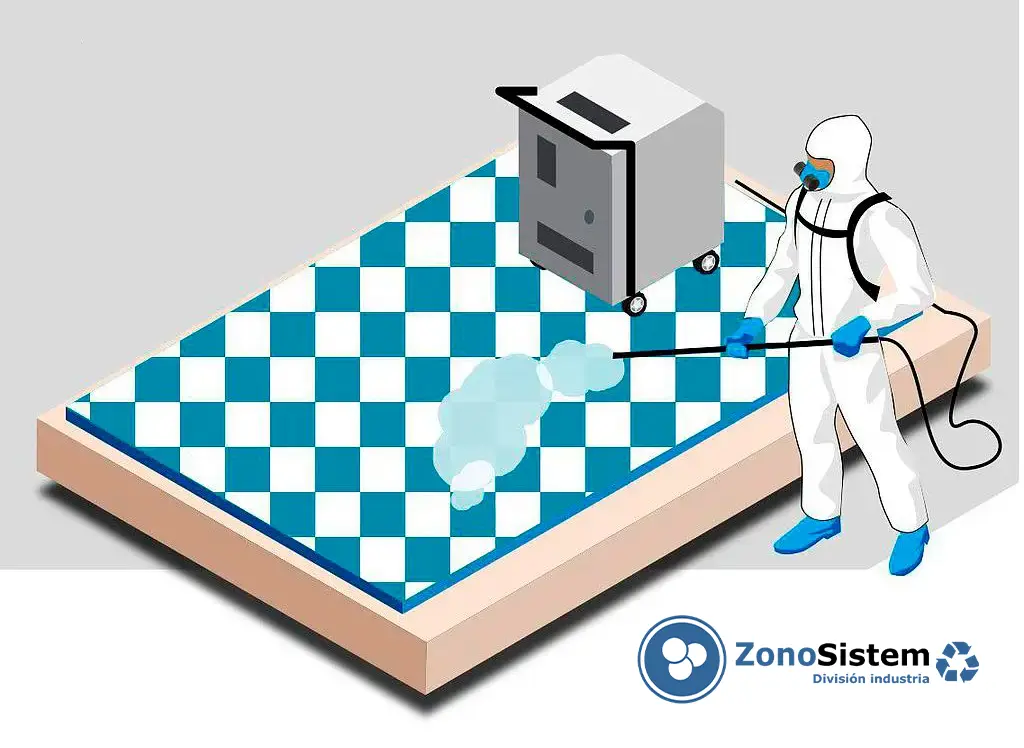
Ozone for surface washing and cleaning
Ozonated water is an excellent biocide for contact disinfection of surfaces in the agri-food industry. It is a very simple tool to use that transforms tap water into disinfectant water with the aim of eliminating any pathogens from surfaces. Furthermore, it reduces the consumption of chemicals and hot water, shortens the time required and reduces the number of rinses, whilst also lowering the quantity and level of contamination in effluent.
Ele não deixa resíduos que possam afetar suas receitas ou produtos, o que proporciona aos clientes ainda mais tranquilidade. Além disso, o ozônio é gerado no local, portanto, não há necessidade de transportá-lo, armazená-lo ou manuseá-lo. O sistema opera de forma totalmente automática e não requer trabalho manual. Com o ozônio, você tem a garantia de desinfecção, com medições em tempo real, ao mesmo tempo em que desfruta de uma economia considerável em comparação com os sistemas tradicionais.
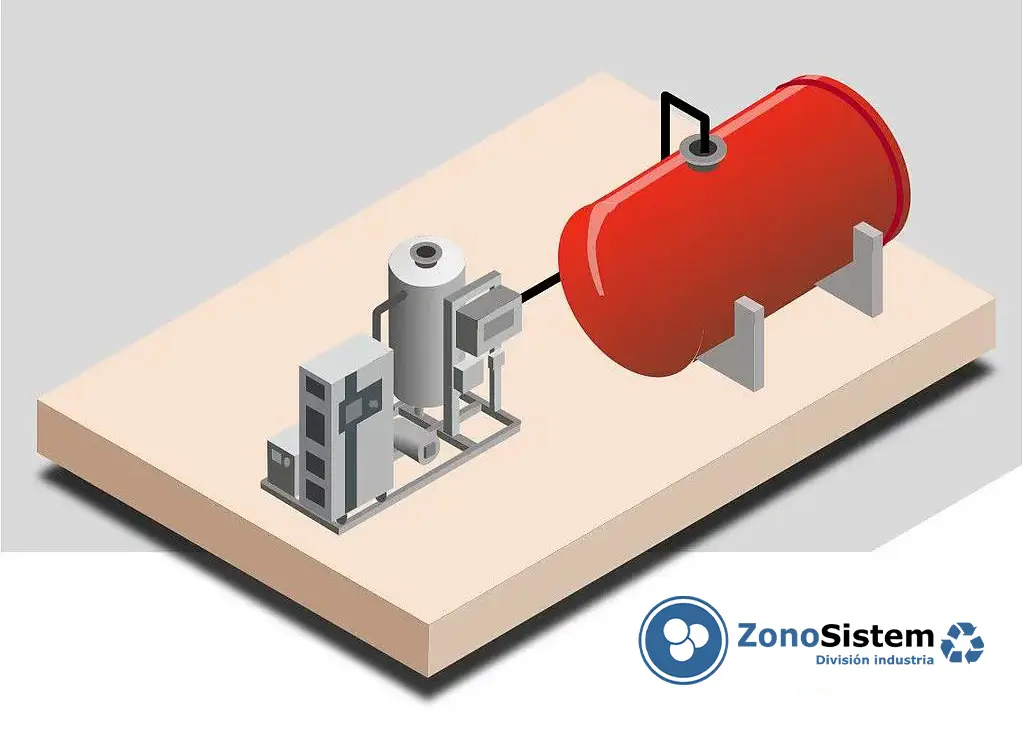
Ozone for fire-fighting water tanks
Fire-fighting tanks are reservoirs of water where dangerous microorganisms such as Legionella can grow and develop, and where biofilm can form in pipes and drainage systems. Chlorine is traditionally the most widely used method of disinfection; however, as it is a packaged chemical, it requires a continuous supply, involving ordering, receipt, storage, precautions against potential spills, transport to the point of use, connection, and so on.
Ozone is a truly effective and efficient method for sanitising and disinfecting tanks, reservoirs, pipework and the water itself. Ozone is generated on-site, so there is no need to transport, store or manage it. The ozone generator extracts oxygen from the air, converts it into ozone using electrical discharges, and injects it into the water in the tank via its injection and contact system. The system simply requires a power socket and needs to be connected to the tank you wish to treat. The system operates fully automatically, without the need for manual labour.
Ozone Treatment in Industrial Water
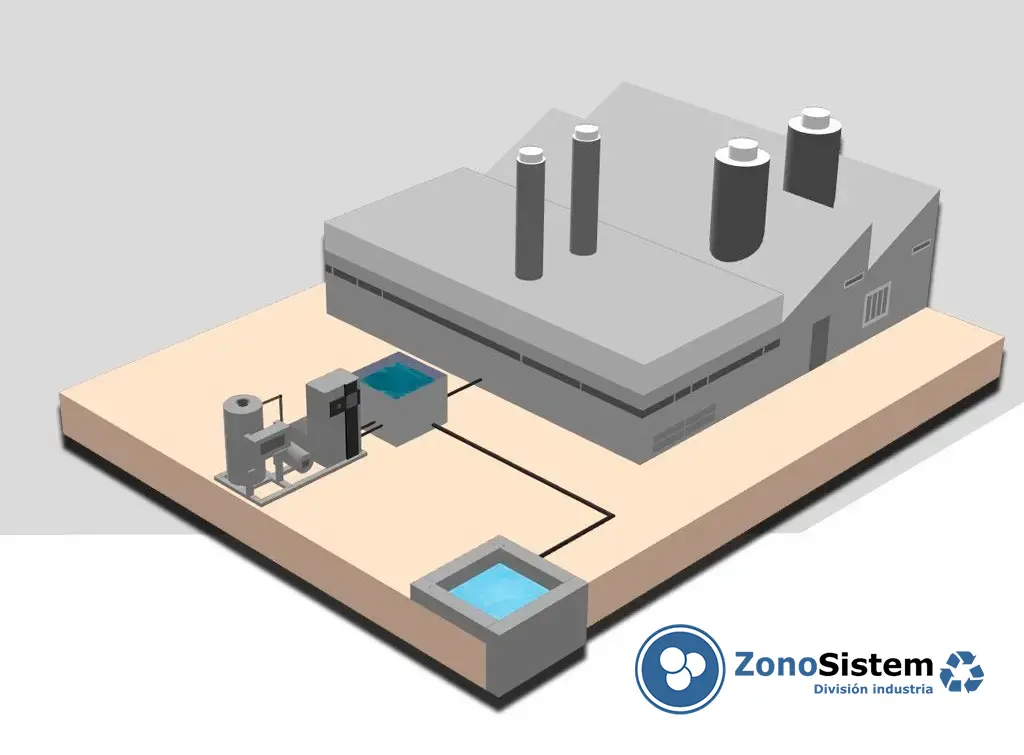
Ozone for industrial DWTP
Ozone is an ideal solution for treating water from the mains supply or from wells prior to industrial use, as its oxidising power enables the removal or reduction of contaminants such as nitrates (from fertilisers and livestock effluent), pesticides, heavy metals, excess amounts of dissolved salts or organic matter that cause turbidity, taste or odours. Furthermore, it is particularly effective against chlorates – by-products of chlorine disinfection – and against chlorinated or brominated anisoles, which are responsible for unwanted odours and tastes that can compromise the quality of the end products. Unlike other disinfectants, ozone acts rapidly and leaves no persistent chemical residues, ensuring purer, safer water that meets the highest industry standards.
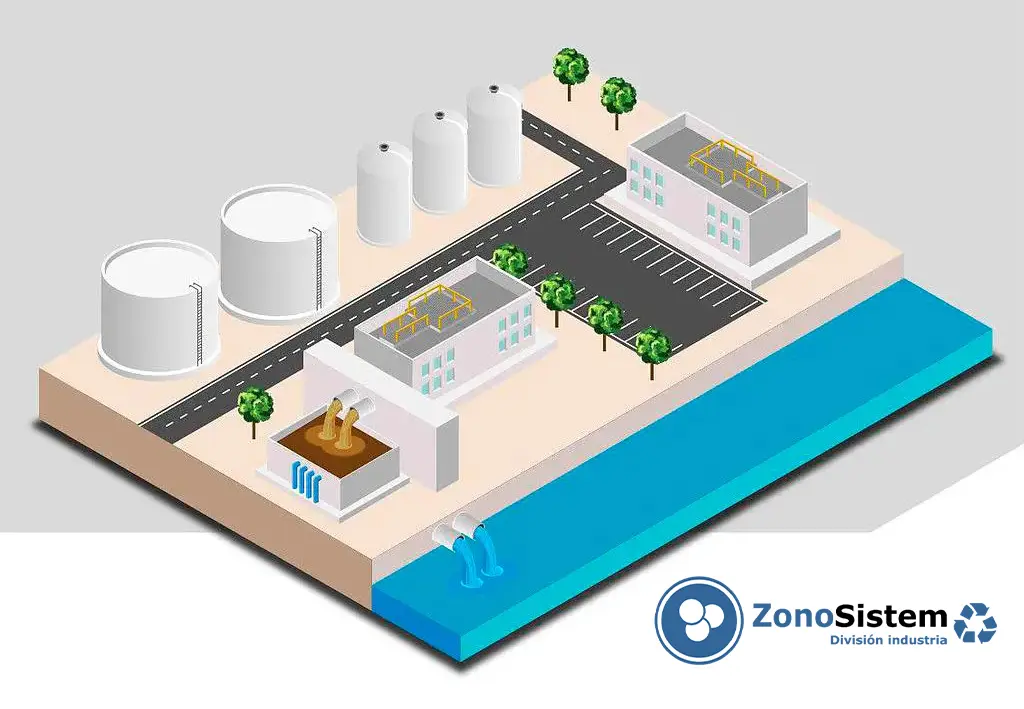
Ozone for industrial WWTPs
Industrial wastewater contains a wide variety of pollutants depending on its source and the type of industry, which can sometimes make it very complex to treat in order to comply with current discharge regulations. Ozone is a well-established technology in WWTPs as it provides a straightforward solution to complex problems. Pre-oxidation of the effluent prior to biological treatment, to improve the COD/BOD ratio. Tertiary treatment for reuse, so that the water can be reused by the industry.
Ozone’s powerful oxidising capacity makes it an excellent tool for use at any of these stages. Ozone is a simple and safe technique that achieves even the most demanding results. ZonoSistem advises detailed engineering firms on the drafting of projects, as well as designing and manufacturing the ozone generators for the actual project.
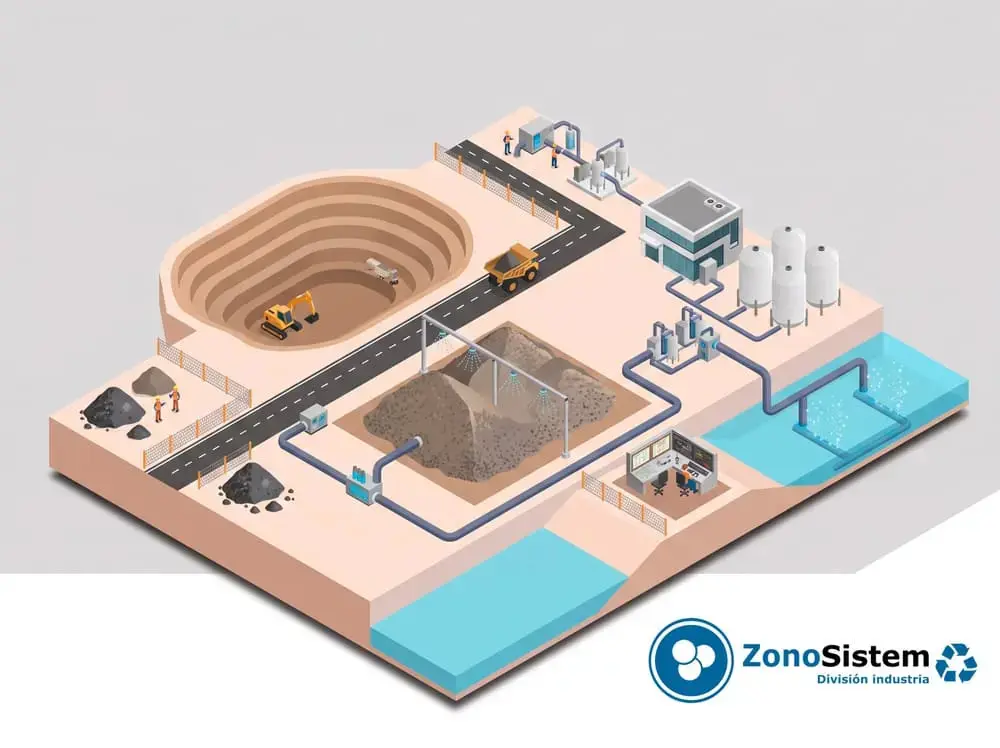
Ozone for mining WWTP
In the mining industry, the quality of the final concentrate directly determines its commercial value. The presence of impurities such as arsenic, iron or residual organic compounds can result in significant financial penalties and reduce the overall efficiency of the process. In this context, ozone (O₃) is an advanced oxidation technology capable of improving flotation selectivity, eliminating residual reagents and facilitating the removal of heavy metals.
The pollutants present in mining processes originate at various stages. Firstly, the ore itself naturally contains complex sulphides such as pyrite (FeS₂), arsenopyrite (FeAsS) and galena (PbS), as well as structural impurities such as arsenic, iron and other trace metals. These species are embedded in the mineral matrix and are difficult to separate completely during the initial stages of the process.
Ozone Treatment in Air
Ozone for NOx oxidation
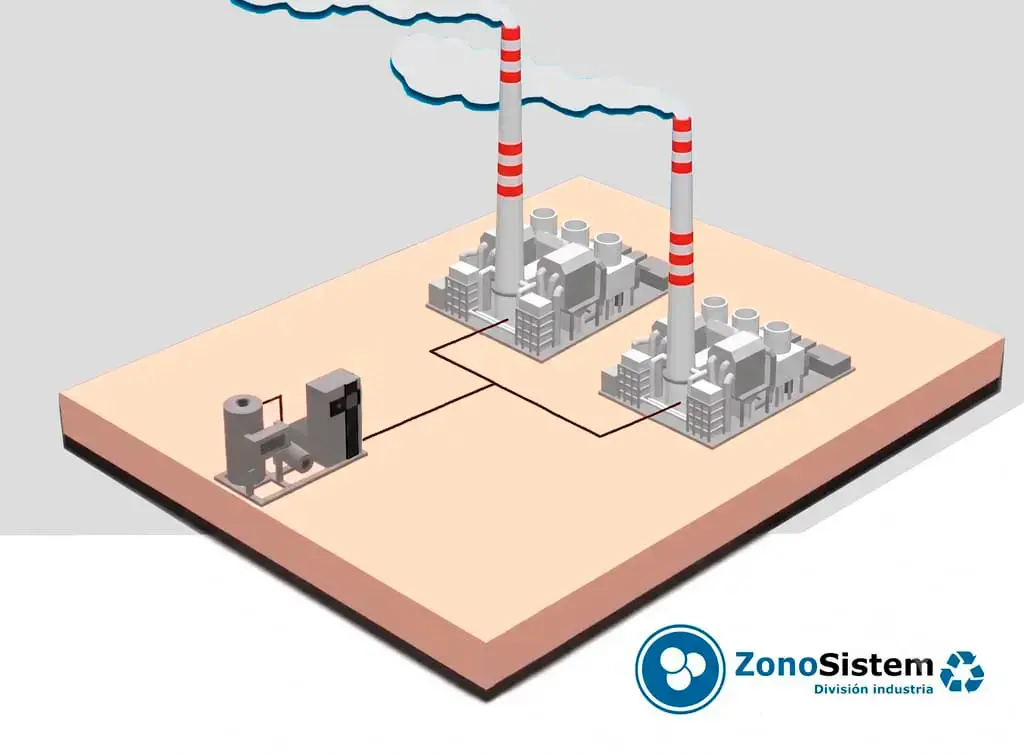
In industrial combustion and incineration plants, the control of nitrogen oxide (NOx) emissions is a key factor in complying with environmental regulations and reducing the impact on the atmosphere. In this context, ozone (O₃) is recognised as an advanced oxidation technology capable of converting NOx into compounds that are more easily removed, thereby improving the efficiency of abatement systems and enabling stricter emission limits to be met in a stable and controlled manner.
ZonoSistem adds value to these solutions, as it designs and manufactures high-output, high-concentration ozone generators, housed in plug-and-play containers to enable rapid installation without the need for civil engineering works.
Ozone for deodorisation towers
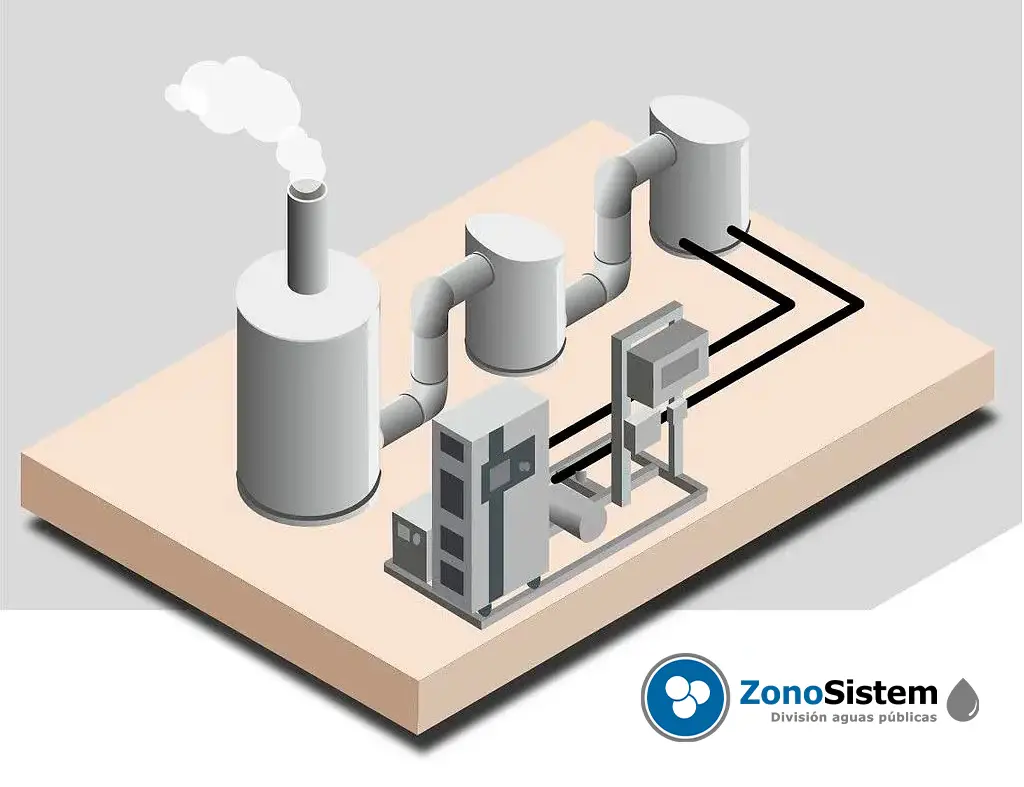
Ozone is a gas used in gas scrubbers and deodorisation towers, primarily to eliminate odours and reduce volatile organic compounds. Ozone has a high oxidation potential, and when injected into the scrubbing tower, it mixes with the gases, reacting with all kinds of chemical compounds, reducing them, oxidising them and transforming them into degraded compounds, resulting in most cases in a significant reduction in odour and volatile organic compounds (VOCs).
It is very easy to install and, furthermore, ozone is neither stored nor transported; it is generated on site from the air we breathe and applied instantly. It operates automatically and requires no manpower. All these advantages make ozone a superb ally for getting the most out of your gas scrubber or deodorisation tower.
Ozone for indoor environments
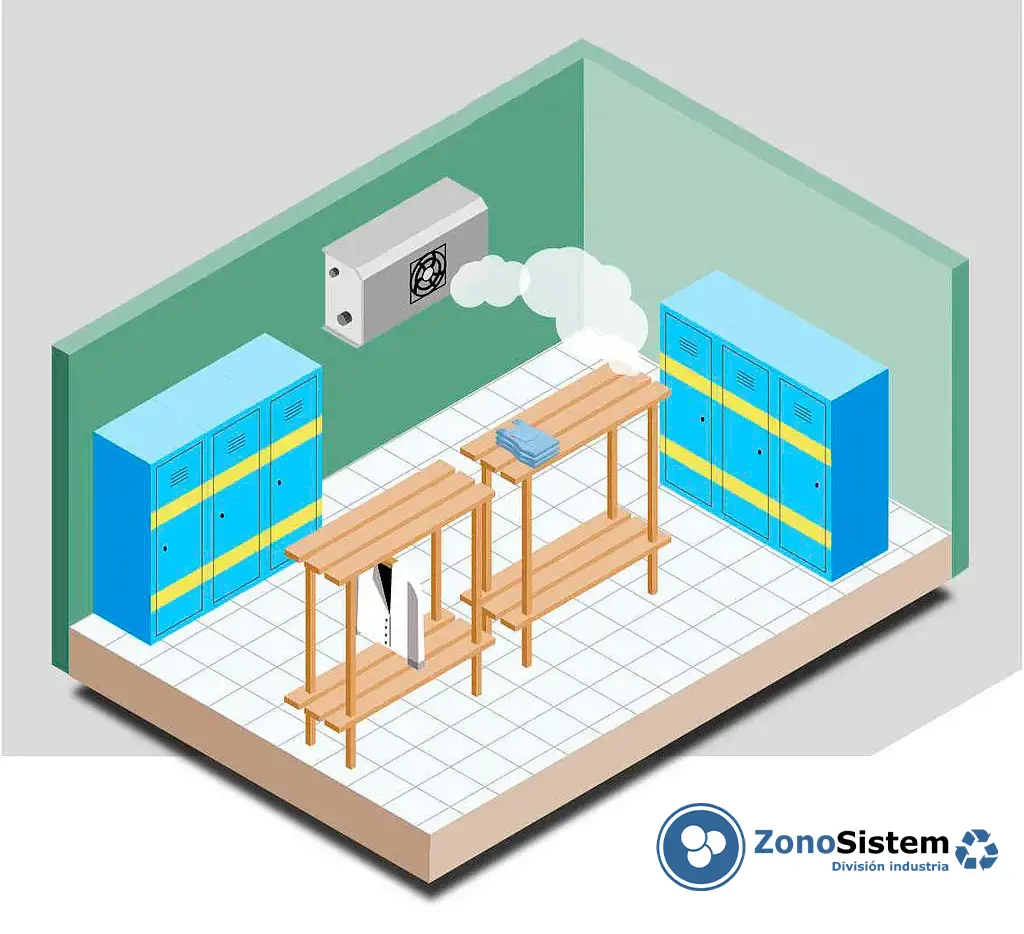
Ozone gas is a powerful purifier and sanitiser for environments and surfaces. Poor ventilation, airborne organic matter and the client’s own industrial activity contribute to contamination of both surfaces and the environment, leading to the build-up of unpleasant odours, viruses and pathogens that affect the quality of the final product.
Ozone quickly disinfects and eliminates odours from rooms, surfaces and fabrics in industrial settings, hotels, hospitals, vehicles, trains, aeroplanes, gyms, offices, etc...
Ozone cannot be used in the presence of people; therefore, we will carry out environmental shock treatments without people present.
Ozone for extractor hoods
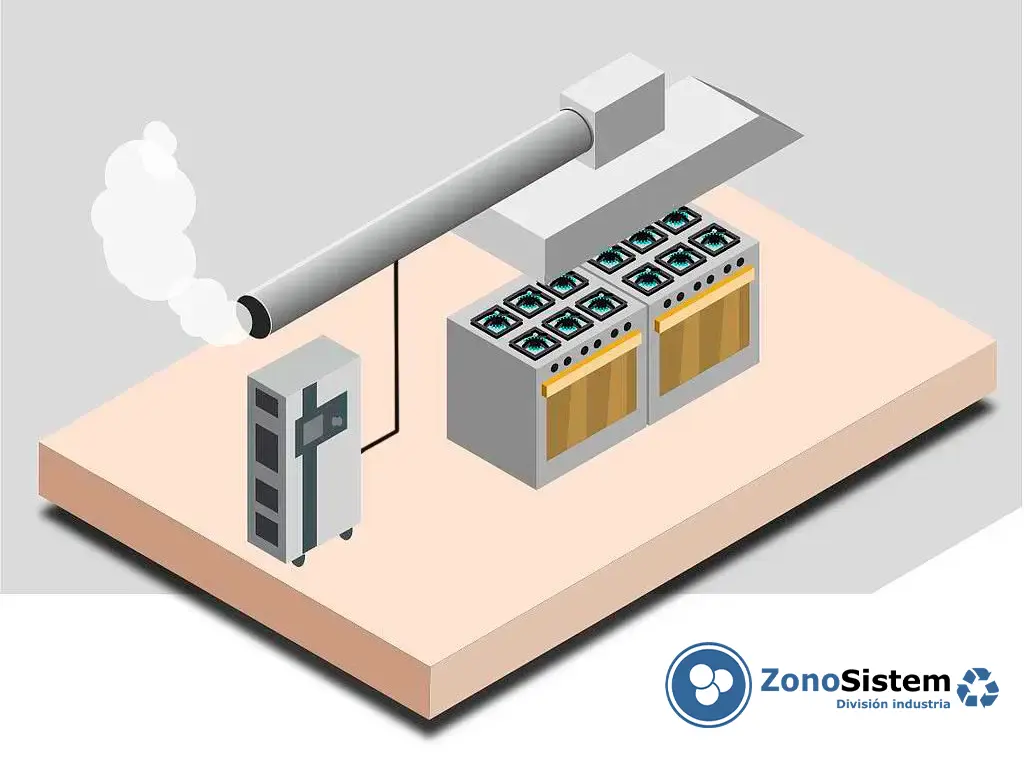
Ozone has become a highly effective solution for the elimination of odours from extractor hoods in restaurant and bar kitchens, thanks to its high efficiency and ease of integration. All that is required is to inject ozone gas into the extractor duct. As it passes through, the ozone reacts with volatile organic compounds (VOCs), transforming them into breakdown products that are odourless and also less polluting. Ozone does not simply mask odours; it literally destroys the compounds that cause them.
Furthermore, ozone is generated on-site; there is no need to transport or store it – it is produced on the spot and applied immediately. These characteristics of ozone, combined with its ease of installation and control and low electricity consumption, make it an excellent tool for reducing the environmental impact and potential nuisance that the hospitality industry may cause in its surroundings.
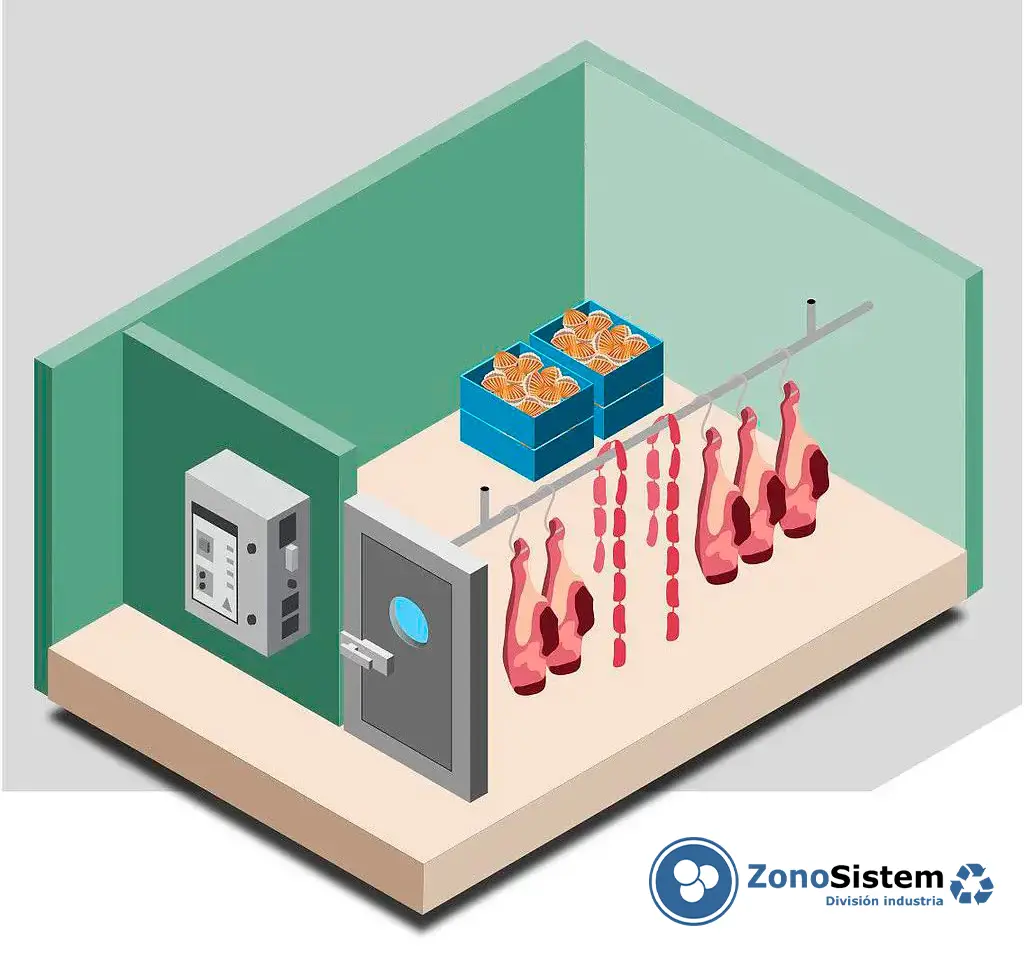
Ozone for cold stores
Ozone is used in cold stores to disinfect the air and surfaces and eliminate unpleasant odours. Ozone is a gas that very quickly and effectively eliminates viruses, bacteria, fungi and mould from the air and surfaces of cold stores, refrigeration units or storage facilities for perishable goods, as well as unpleasant odours. The ozone generator produces ozone on-site and releases it into the cold store immediately. The ozone system operates automatically and is easy to install.
These advantages make ozone a powerful tool for sanitising cold stores automatically and easily, without the need for manual labour. In the case of fruit and vegetable storage, ozone also breaks down ethylene, preventing fruit and vegetables from ripening too quickly.